A Byproduct That Becomes an Operational Problem

Triazine scavengers are highly effective at removing H2S from sour gas and crude streams, but the reaction that makes them effective also produces a byproduct that can create its own operational headache. As triazine reacts with H2S, it forms dithiazine, a cyclic compound that is only sparingly soluble in water and hydrocarbon phases. Under the wrong conditions, dissolved dithiazine falls out of solution and deposits as a sticky, waxy solid on pipe walls, valves, and separator internals.

These deposits are more than a nuisance. Accumulated dithiazine scale can restrict flow, foul instrumentation, plug small-bore piping, and in some cases contribute to under-deposit corrosion by trapping moisture and other corrosive species against the pipe wall.

Why Dithiazine Falls Out of Solution

Dithiazine solubility is sensitive to temperature, pH, and the ratio of triazine to H2S in the treated stream. As treated fluid cools while moving downstream, dithiazine that was dissolved at higher wellhead temperatures can exceed its solubility limit and precipitate. Overtreating with triazine, meaning dosing well beyond what is needed to react with the H2S present, increases the pool of unreacted triazine and reaction byproduct available to deposit, since excess triazine does not simply disappear once H2S demand is satisfied.

Water cut and pH also play a role. Dithiazine tends to be more soluble in lower-pH conditions and less soluble as pH rises, which means the same treatment program can behave differently in a high water-cut stream than in a mostly hydrocarbon stream, even at identical triazine dosage.

Where Deposits Tend to Form

Dithiazine scale is most commonly reported at points where flow velocity drops and temperature falls, such as low-flow sections of gathering lines, the bottoms of separators and tanks, and dead-leg piping where treated fluid sits with little movement. Chokes, control valves, and other restrictions can also see accelerated buildup because of the combination of pressure drop, temperature drop, and turbulence at those locations.

Operators sometimes discover the problem indirectly, through unexplained pressure drop across a section of line, reduced separator efficiency, or plugged sample points, before identifying dithiazine as the cause through solids analysis.

Managing and Preventing Buildup

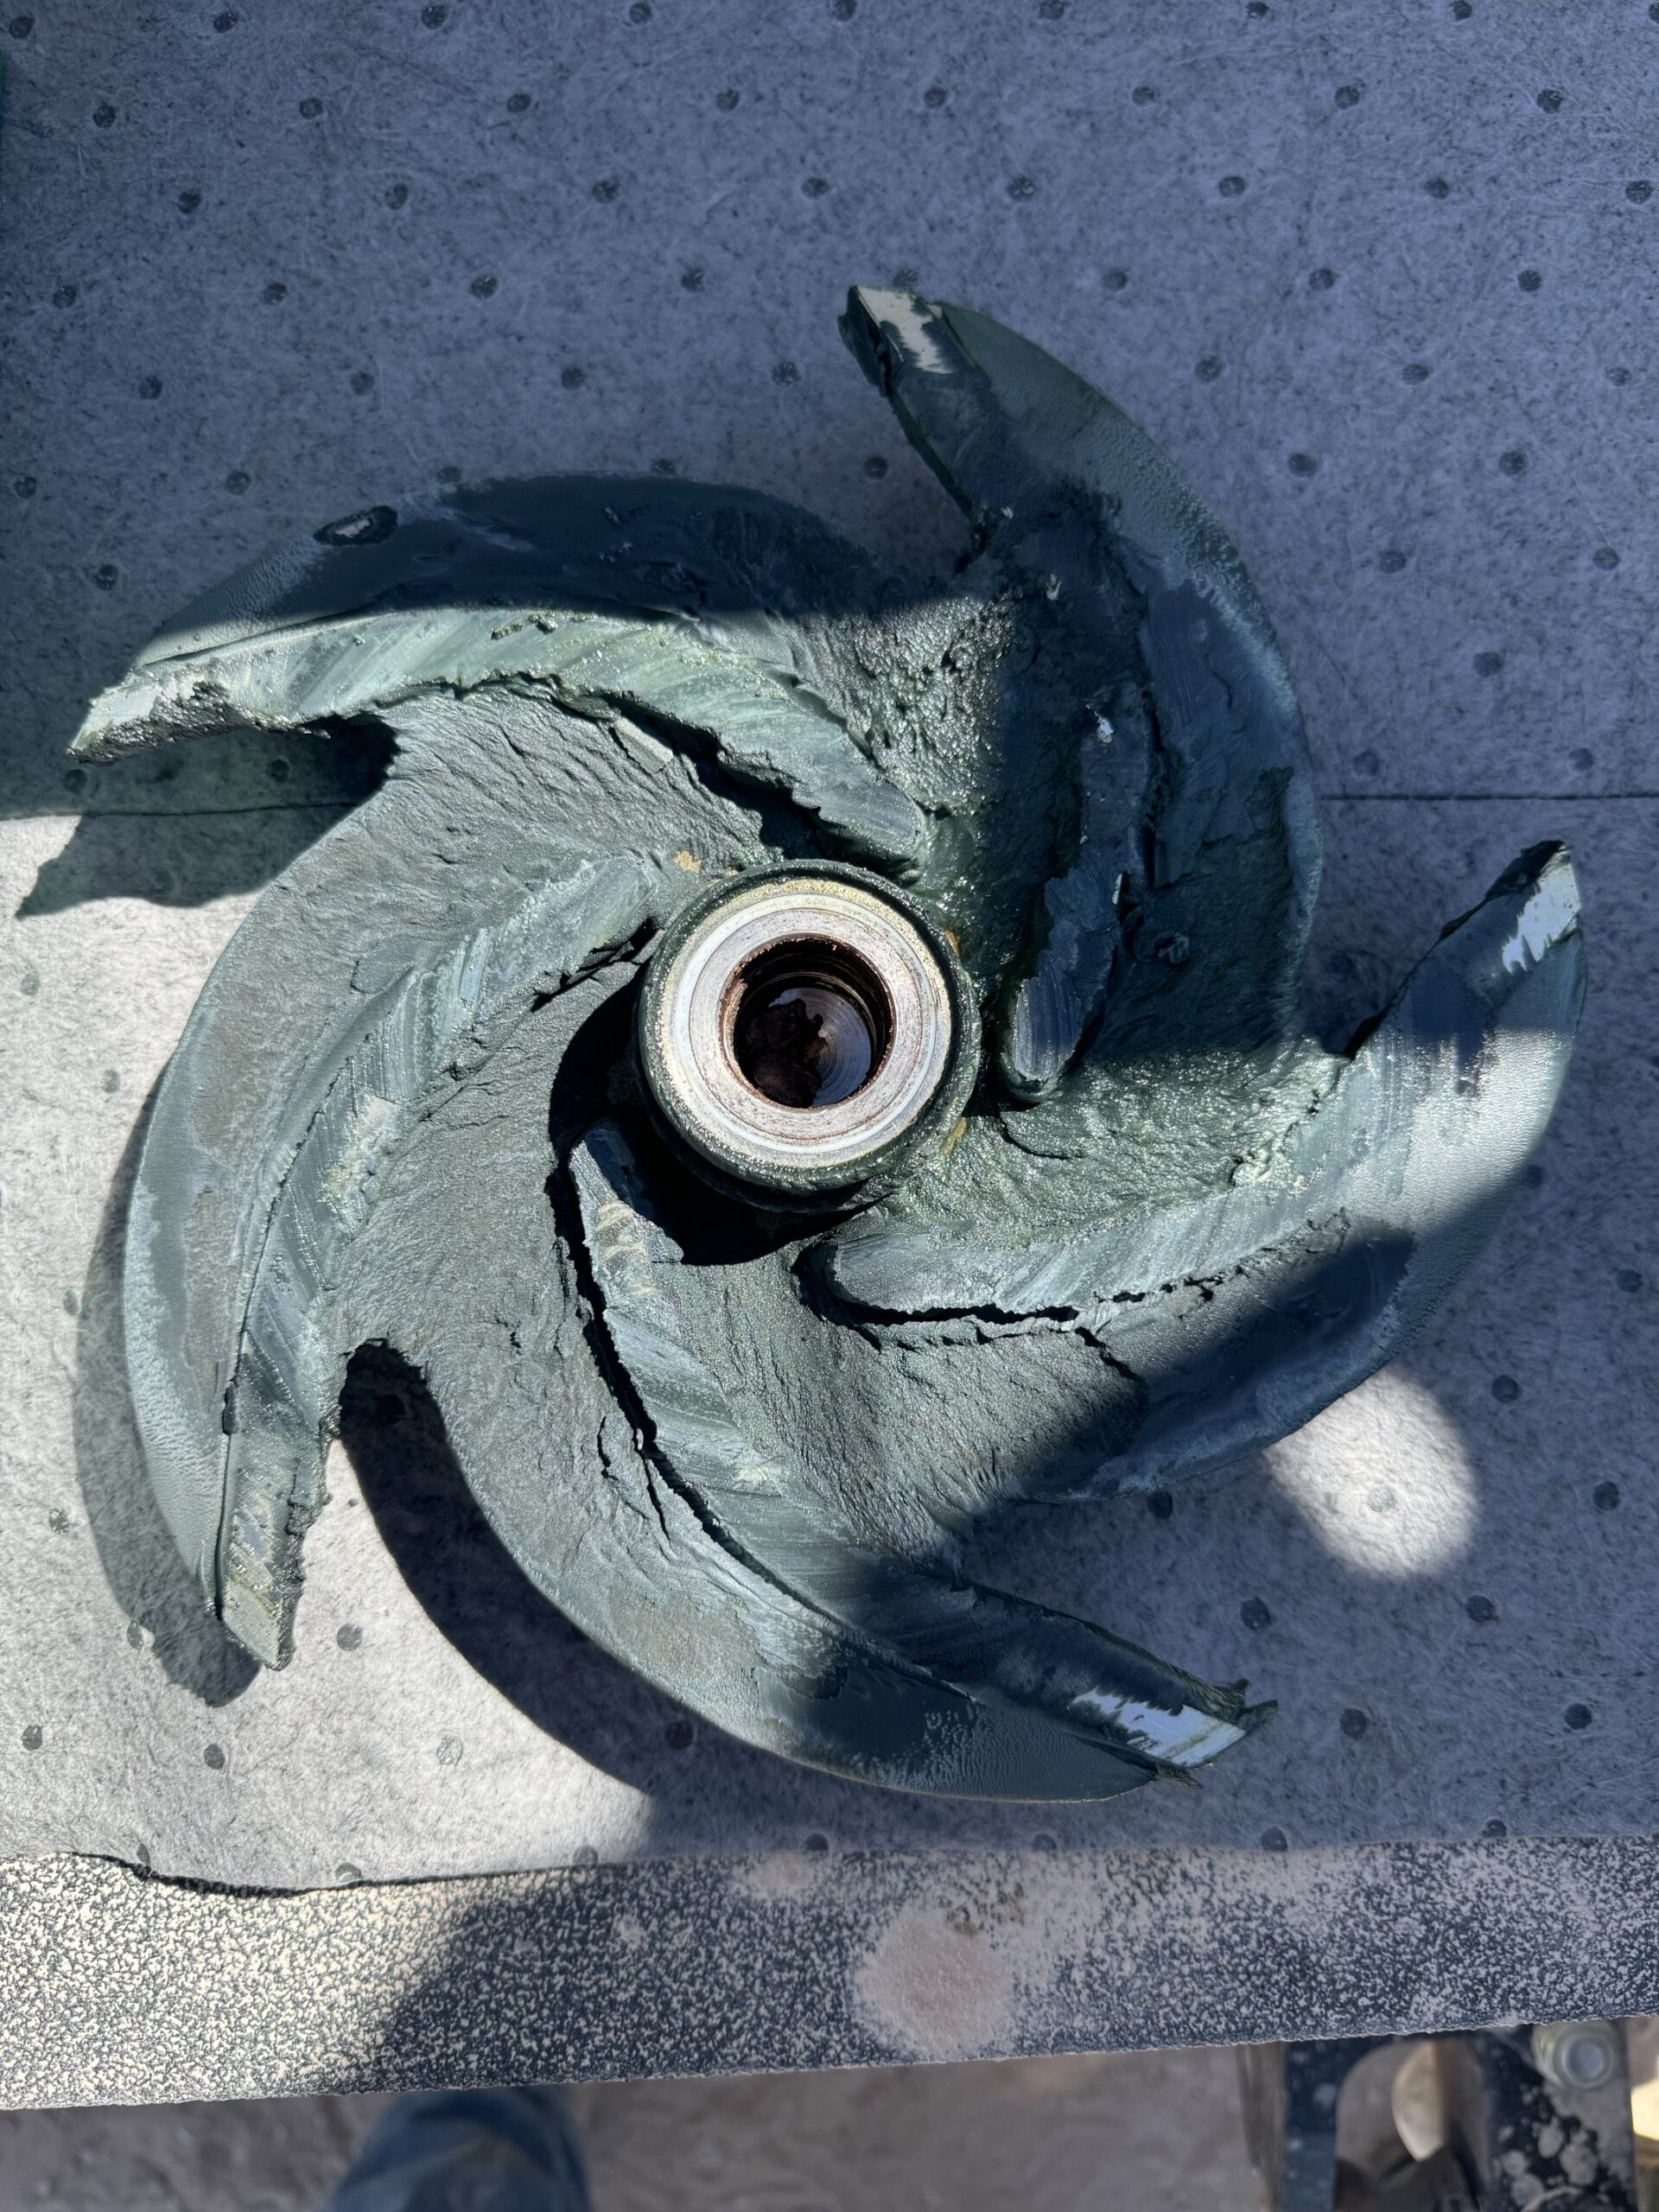
Crude oil pipeline with blockage from triazine

The most direct prevention strategy is dosing triazine as close as practical to the stoichiometric demand of the H2S present, rather than applying a flat excess as a safety margin. Regular H2S monitoring and dosage adjustment, rather than a fixed injection rate, reduces the amount of unreacted triazine and dithiazine byproduct moving through the system.

Where deposits have already formed, mechanical cleaning, solvent washes, and periodic pigging are the common remediation approaches. Some operators also adjust injection location to allow more reaction and residence time upstream of the points where deposits have historically formed, giving the byproduct a chance to remain in solution through the coolest part of the system rather than concentrating at a single low point.

A Reminder About Treatment Tradeoffs

Dithiazine formation is a useful reminder that scavenger chemistry does not eliminate sulfur from a system, it converts it into a different form. Effective H2S management means tracking where that converted sulfur goes, not just confirming that H2S readings at the wellhead have dropped.

Diagnosing Suspected Dithiazine Deposits

When operators suspect dithiazine is behind a plugging or pressure-drop issue, solids sampling and laboratory analysis are the most reliable way to confirm it rather than assuming based on location alone, since paraffin, scale, and other deposit types can produce similar symptoms. A simple visual inspection can be misleading, as dithiazine deposits can range from a soft, waxy film to a harder, more crystalline solid depending on how long they have accumulated and what other materials have co-deposited with them.

Where lab analysis confirms dithiazine, reviewing recent injection rates and H2S trend data for the affected line often reveals whether the root cause was a period of overtreatment, a drop in flow velocity, a temperature change, or some combination of the three, which helps target the fix rather than simply cleaning the line and waiting for the deposit to return.

Longer-Term Program Adjustments

Operators who repeatedly deal with dithiazine buildup at the same locations sometimes find it worthwhile to reconsider scavenger chemistry entirely, moving to a non-triazine alternative for that specific segment of the system, rather than continuing to manage the byproduct of a triazine program through cleaning cycles. This is a bigger step than adjusting dosage or injection point, but it can be the more cost-effective long-term solution where deposits recur despite optimized dosing.

Working With Solvent and Dispersant Suppliers

For lines with established dithiazine deposit history, some operators add periodic solvent treatments as a preventive measure rather than waiting for a plugging event to trigger remediation. Working with a chemical supplier familiar with dithiazine solubility behavior can help identify a solvent or dispersant compatible with both the deposit and the produced fluid, since a solvent effective on paraffin or asphaltene deposits is not necessarily effective on a dithiazine-dominated deposit, and testing compatibility before a full-scale treatment avoids wasted time and chemical cost.

A Byproduct That Becomes an Operational Problem

Triazine scavengers are highly effective at removing H2S from sour gas and crude streams, but the reaction that makes them effective also produces a byproduct that can create its own operational headache. As triazine reacts with H2S, it forms dithiazine, a cyclic compound that is only sparingly soluble in water and hydrocarbon phases. Under the wrong conditions, dissolved dithiazine falls out of solution and deposits as a sticky, waxy solid on pipe walls, valves, and separator internals.

These deposits are more than a nuisance. Accumulated dithiazine scale can restrict flow, foul instrumentation, plug small-bore piping, and in some cases contribute to under-deposit corrosion by trapping moisture and other corrosive species against the pipe wall.

Why Dithiazine Falls Out of Solution

Dithiazine solubility is sensitive to temperature, pH, and the ratio of triazine to H2S in the treated stream. As treated fluid cools while moving downstream, dithiazine that was dissolved at higher wellhead temperatures can exceed its solubility limit and precipitate. Overtreating with triazine, meaning dosing well beyond what is needed to react with the H2S present, increases the pool of unreacted triazine and reaction byproduct available to deposit, since excess triazine does not simply disappear once H2S demand is satisfied.

Water cut and pH also play a role. Dithiazine tends to be more soluble in lower-pH conditions and less soluble as pH rises, which means the same treatment program can behave differently in a high water-cut stream than in a mostly hydrocarbon stream, even at identical triazine dosage.

Where Deposits Tend to Form

Dithiazine scale is most commonly reported at points where flow velocity drops and temperature falls, such as low-flow sections of gathering lines, the bottoms of separators and tanks, and dead-leg piping where treated fluid sits with little movement. Chokes, control valves, and other restrictions can also see accelerated buildup because of the combination of pressure drop, temperature drop, and turbulence at those locations.

Operators sometimes discover the problem indirectly, through unexplained pressure drop across a section of line, reduced separator efficiency, or plugged sample points, before identifying dithiazine as the cause through solids analysis.

Managing and Preventing Buildup

Crude oil pipeline with blockage from triazine

The most direct prevention strategy is dosing triazine as close as practical to the stoichiometric demand of the H2S present, rather than applying a flat excess as a safety margin. Regular H2S monitoring and dosage adjustment, rather than a fixed injection rate, reduces the amount of unreacted triazine and dithiazine byproduct moving through the system.

Where deposits have already formed, mechanical cleaning, solvent washes, and periodic pigging are the common remediation approaches. Some operators also adjust injection location to allow more reaction and residence time upstream of the points where deposits have historically formed, giving the byproduct a chance to remain in solution through the coolest part of the system rather than concentrating at a single low point.

A Reminder About Treatment Tradeoffs

Dithiazine formation is a useful reminder that scavenger chemistry does not eliminate sulfur from a system, it converts it into a different form. Effective H2S management means tracking where that converted sulfur goes, not just confirming that H2S readings at the wellhead have dropped.

Diagnosing Suspected Dithiazine Deposits

When operators suspect dithiazine is behind a plugging or pressure-drop issue, solids sampling and laboratory analysis are the most reliable way to confirm it rather than assuming based on location alone, since paraffin, scale, and other deposit types can produce similar symptoms. A simple visual inspection can be misleading, as dithiazine deposits can range from a soft, waxy film to a harder, more crystalline solid depending on how long they have accumulated and what other materials have co-deposited with them.

Where lab analysis confirms dithiazine, reviewing recent injection rates and H2S trend data for the affected line often reveals whether the root cause was a period of overtreatment, a drop in flow velocity, a temperature change, or some combination of the three, which helps target the fix rather than simply cleaning the line and waiting for the deposit to return.

Longer-Term Program Adjustments

Operators who repeatedly deal with dithiazine buildup at the same locations sometimes find it worthwhile to reconsider scavenger chemistry entirely, moving to a non-triazine alternative for that specific segment of the system, rather than continuing to manage the byproduct of a triazine program through cleaning cycles. This is a bigger step than adjusting dosage or injection point, but it can be the more cost-effective long-term solution where deposits recur despite optimized dosing.

Working With Solvent and Dispersant Suppliers

For lines with established dithiazine deposit history, some operators add periodic solvent treatments as a preventive measure rather than waiting for a plugging event to trigger remediation. Working with a chemical supplier familiar with dithiazine solubility behavior can help identify a solvent or dispersant compatible with both the deposit and the produced fluid, since a solvent effective on paraffin or asphaltene deposits is not necessarily effective on a dithiazine-dominated deposit, and testing compatibility before a full-scale treatment avoids wasted time and chemical cost.

When introduced into a stream afflicted with H2S, the hemiformal decomposes to release formaldehyde, which then reacts with hydrogen sulfide to form stable, non-volatile byproducts such as thiomethylene glycol.  The reaction is typically fast and efficient, particularly in aqueous or mixed-phase environments. Unlike some traditional scavengers, hemiformal can maintain activity across a broad pH range and is less likely to generate problematic solids. When considering if hemiformal is the right product, certain operating conditions are reviewed, such as pH and temperature.

Heading 1

When introduced into a stream afflicted with H2S, the hemiformal decomposes to release formaldehyde, which then reacts with hydrogen sulfide to form stable, non-volatile byproducts such as thiomethylene glycol.  The reaction is typically fast and efficient, particularly in aqueous or mixed-phase environments. Unlike some traditional scavengers, hemiformal can maintain activity across a broad pH range and is less likely to generate problematic solids. When considering if hemiformal is the right product, certain operating conditions are reviewed, such as pH and temperature.

Heading 2

When introduced into a stream afflicted with H2S, the hemiformal decomposes to release formaldehyde, which then reacts with hydrogen sulfide to form stable, non-volatile byproducts such as thiomethylene glycol.  The reaction is typically fast and efficient, particularly in aqueous or mixed-phase environments. Unlike some traditional scavengers, hemiformal can maintain activity across a broad pH range and is less likely to generate problematic solids. When considering if hemiformal is the right product, certain operating conditions are reviewed, such as pH and temperature.

Heading 3

Heading 4

When introduced into a stream afflicted with H2S, the hemiformal decomposes to release formaldehyde, which then reacts with hydrogen sulfide to form stable, non-volatile byproducts such as thiomethylene glycol.  The reaction is typically fast and efficient, particularly in aqueous or mixed-phase environments. Unlike some traditional scavengers, hemiformal can maintain activity across a broad pH range and is less likely to generate problematic solids. When considering if hemiformal is the right product, certain operating conditions are reviewed, such as pH and temperature. 

Key Benefits:

  • Controlled formaldehyde release 
  • Lower vapor pressure and improved safety profile 
  • Broad applicability across liquid and gas-phase systems 
  • Reduced scaling in sour water stripping and other high-temp operations 
  • Hemiformal can make the scavenger safe for transport as it is a very stable compound 

Heading 5

Hemiformal is used in a variety of upstream and midstream applications, including: 

  • Gas sweetening systems 
  • Produced water treatment 
  • Crude oil storage and transport 
  • Sour water stripper overheads 
  • Temporary H2S mitigation during maintenance or turnaround

Its adaptability makes it especially useful in operations where system conditions fluctuate or where traditional triazine-based products may underperform. 

Heading 6

While hemiformal offers many advantages, it is not a one-size-fits-all solution. The rate of formaldehyde release can vary depending on formulation and environmental conditions. Additionally, while safer than raw formaldehyde, hemiformal must still be handled with care and appropriate PPE. 

For optimal results, formulation expertise and application-specific customization are key—something we at Q2 Technologies excel at delivering. 

Related Blogs

FAQs

  1. What is dithiazine and how does it form?

    Dithiazine is a reaction byproduct formed when triazine reacts with H₂S. Under certain conditions, the dithiazine can become insoluble and precipitate from the treated stream, forming deposits on pipeline walls and equipment.


  2. Why does dithiazine deposit in pipelines?

    Dithiazine deposits when its concentration exceeds its solubility in the produced fluid. Cooling temperatures, reduced flow velocity, changing water content, pH, and excessive triazine dosing can all contribute to precipitation and buildup.


  3. How can operators prevent dithiazine scale?

    The primary approach is to optimize triazine dosage based on actual H₂S demand rather than consistently overdosing. Monitoring H₂S, adjusting injection rates and locations, and evaluating temperature and flow conditions can reduce the amount of dithiazine carried downstream.


  4. How do you remove existing dithiazine deposits?

    Depending on the severity and location of the deposit, operators may use mechanical cleaning, pigging, solvent treatments, or dispersants. Because dithiazine deposits can resemble paraffin, scale, or other solids, laboratory analysis is recommended before selecting a remediation treatment.

Related Articles