

A single odor call can signal anything from a temporary process upset to a treatment failure that affects safety, compliance, and community trust. To manage sulfide odor complaints effectively, industrial operators need more than a deodorizing response. They need a repeatable process that identifies the source, verifies conditions in the field, stabilizes treatment, and documents what changed.
Hydrogen sulfide and mercaptan odors are especially challenging because people can detect them at very low concentrations. An odor event may generate legitimate concern even when a site is operating below an exposure limit or permit threshold. That does not make the complaint less operationally relevant. Repeated complaints can indicate changing feed conditions, poor containment, inadequate scavenger performance, vapor releases, or a gap between process monitoring and actual site conditions.
Start With a Disciplined Complaint Response
The first response should be prompt, factual, and structured. Record the caller’s location, time, odor description, weather conditions if available, and whether the odor was intermittent or continuous. A complaint reported at the fence line during a specific wind direction provides more useful information than a general report that the facility “smells bad.”
Do not assume the reported location is the source. Terrain, building layouts, temperature inversions, wind shifts, and drainage pathways can carry sulfur odors well beyond the release point. The goal is to correlate the complaint with operating data, field observations, and potential emission pathways.
At the same time, treat a credible H2S concern as a safety matter. Odor is not a reliable personal exposure monitor. At higher concentrations, H2S can impair a person’s sense of smell, creating a dangerous false impression that conditions have improved. Site personnel should follow the facility’s established H2S safety procedures, use appropriate gas detection, and avoid relying on odor intensity to judge risk.
Confirm the Source Before Changing the Chemistry
A common mistake is increasing chemical dosage before confirming why the odor developed. More product may temporarily suppress symptoms, but it can also raise treatment cost while leaving the underlying release pathway unchanged.
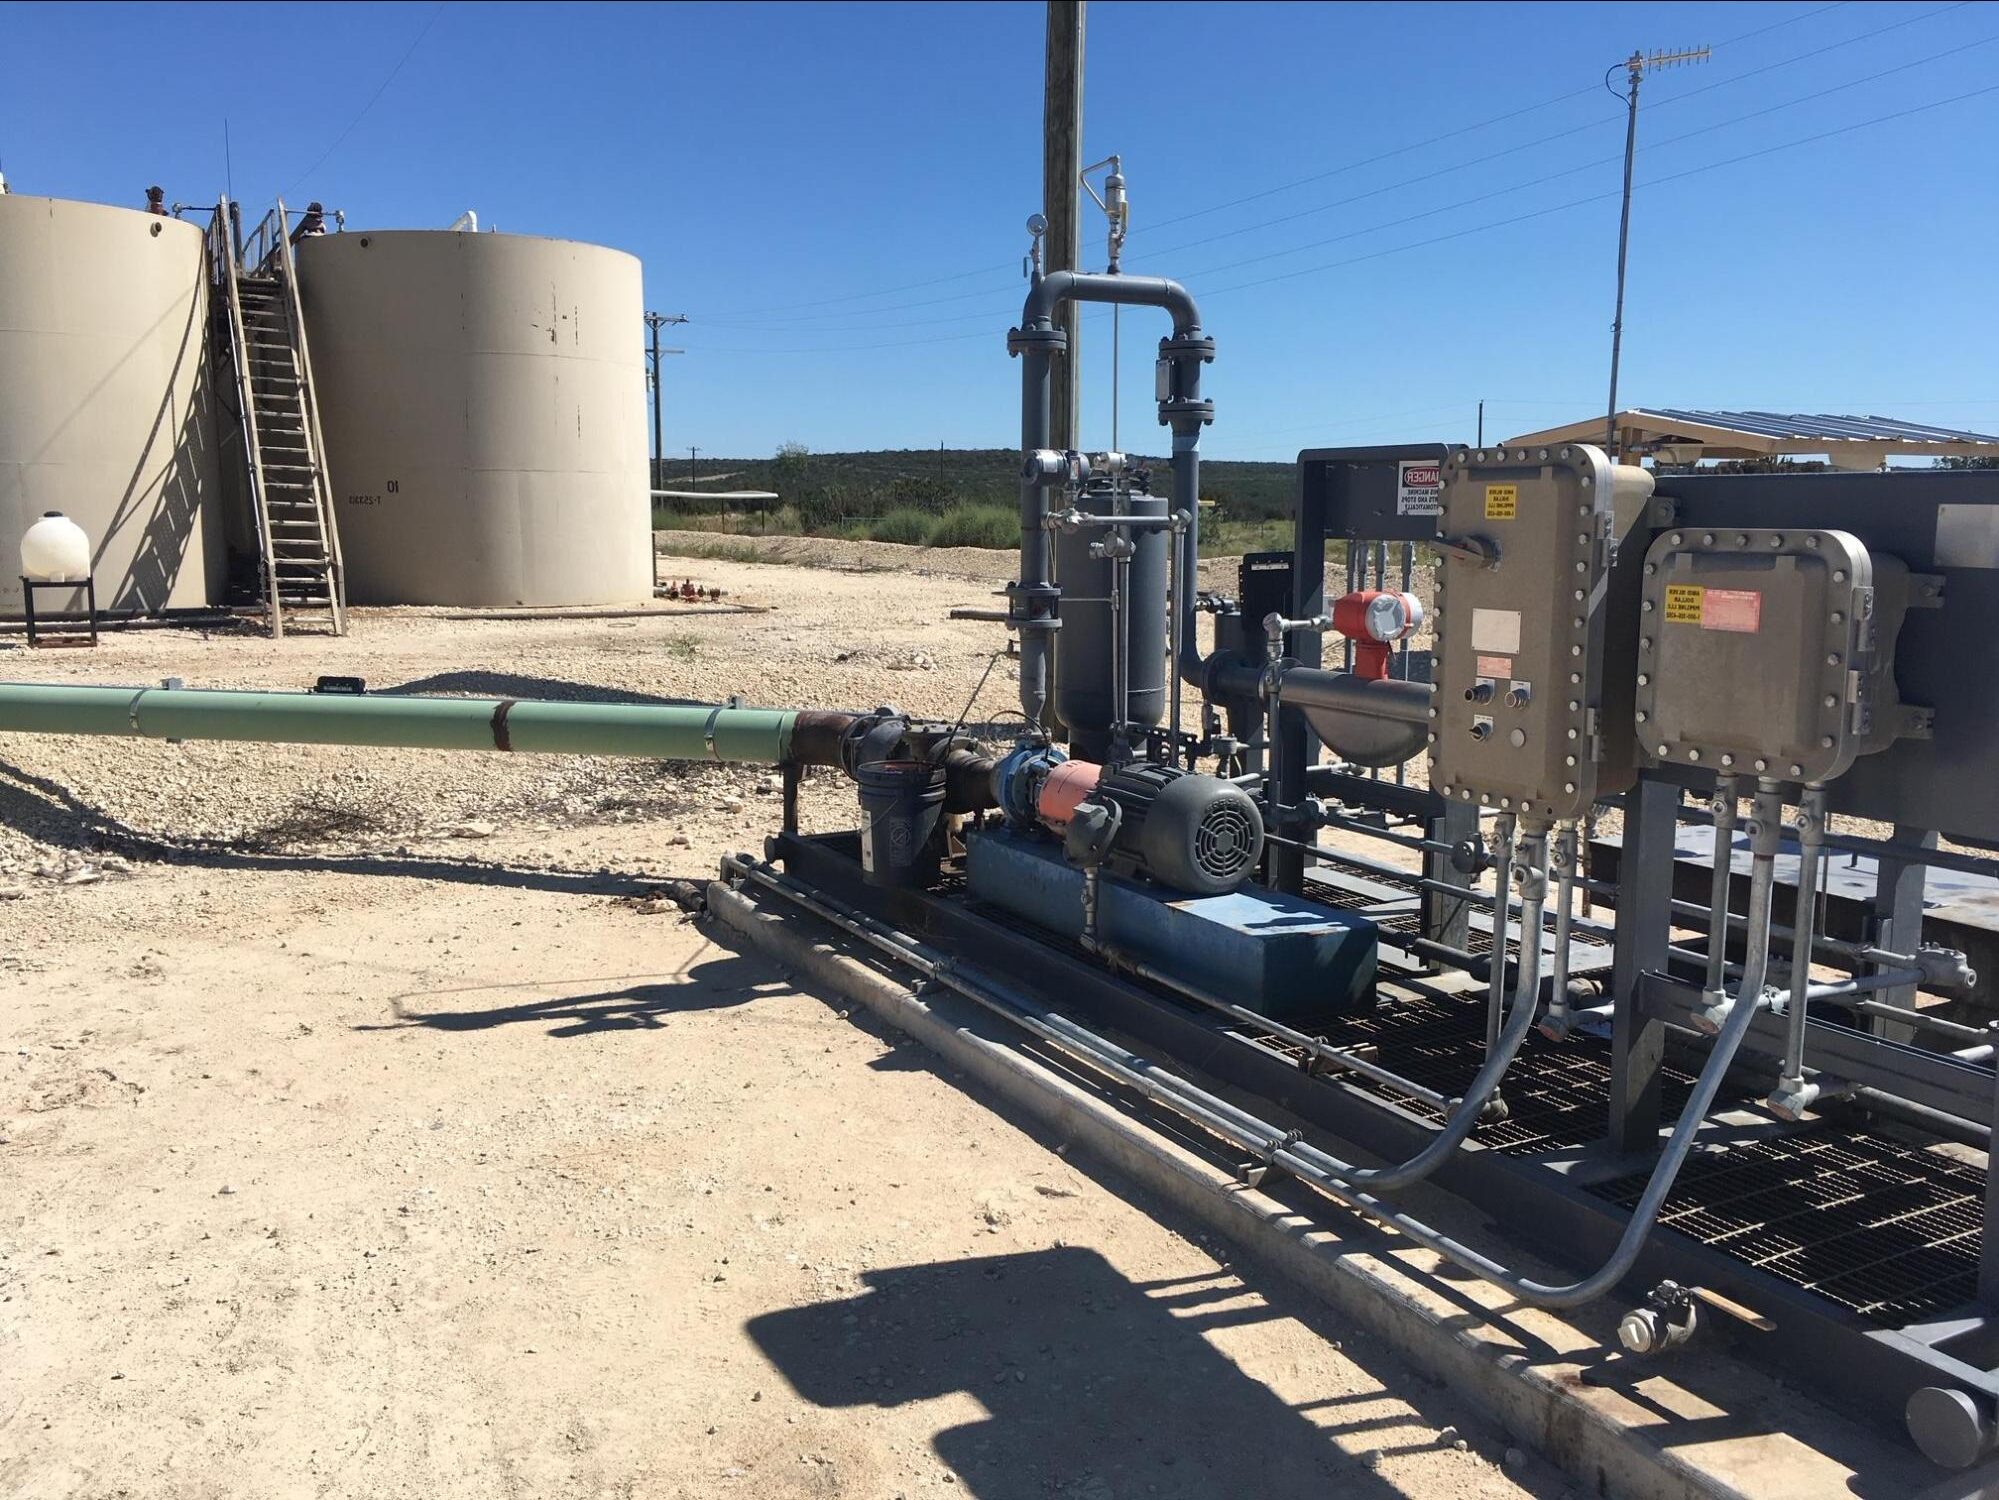
Begin with a source review across the process. In wastewater systems, inspect headworks, equalization basins, lift stations, sludge handling areas, covered process vessels, and ventilation exhaust points. In oil and gas operations, evaluate tank vents, produced-water handling, separators, flare headers, truck-loading areas, vapor recovery equipment, and chemical injection locations. For landfill gas and biogas facilities, inspect condensate management, collection well performance, blower stations, gas treatment equipment, and exposed leachate or digestate areas.
Field measurements should be taken where they can distinguish source strength from transport conditions. Fixed monitors, handheld instruments, liquid-phase sampling, gas analysis, and inspection of seals or vents each answer different questions. A low reading at one process point does not rule out a short-duration release elsewhere. Similarly, high sulfide concentration in a liquid stream does not automatically explain an off-site odor unless volatilization and air movement are considered.
Look for the operating change
Most odor events follow a change, even if the change was not obvious at first. Review recent throughput, temperature, pH, retention time, sulfur loading, chemical delivery records, injection rates, equipment maintenance, and weather. A new well connection, altered crude quality, higher organic loading, reduced aeration, or a failed pump can quickly change sulfide generation or release behavior.
This review should include treatment residence time and mixing. A scavenger or odor-control chemistry may be appropriate for the contaminant but underperform if it is injected too late, poorly mixed, or exposed to a sudden increase in sulfur loading. Application engineering matters as much as product selection.
Match Treatment to the Actual Odor Mechanism
Sulfide odor control is not one problem with one answer. The right treatment depends on whether the priority is removing H2S from a gas stream, controlling dissolved sulfides in water, reducing odor from a surface or ventilation point, or treating mercaptans and other sulfur compounds that may persist after H2S is addressed.
For gas streams, scavenger selection must account for concentration, flow variability, pressure, temperature, required outlet specification, contact time, and spent-product handling. An underdosed treatment system may allow breakthrough during peak loads. An oversized or poorly controlled program may consume chemical without producing a proportional performance benefit.
For liquid systems, treatment must consider pH, dissolved sulfide concentration, organic demand, solids, mixing energy, and the likelihood of H2S stripping into the vapor phase. In some cases, controlling sulfide formation upstream is more effective than treating odors after they are released. In others, targeted treatment at a known odor source provides the fastest operational improvement.
Mercaptans require separate attention. Their odor character can remain noticeable after H2S levels decline, and not every H2S treatment chemistry is designed to control mercaptans effectively. When odor complaints persist despite acceptable H2S results, broader sulfur-species testing can prevent operators from chasing the wrong variable.
Use Monitoring to Control Variability, Not Just Document It
Periodic sampling can confirm performance, but odor complaints often arise during brief upsets that a routine grab sample misses. Continuous or more frequent monitoring can reveal the operating pattern behind those events: a recurring batch discharge, a nighttime temperature shift, a tank pressure cycle, or a chemical injection interruption.
The most useful monitoring programs connect data to decisions. Establish practical action levels for sulfur concentration, odor-related process indicators, treatment consumption, and equipment status. When an action level is reached, the response should be clear: inspect a pump, verify inventory, increase sampling, adjust injection within approved operating limits, or investigate a defined process area.
Automation can improve consistency, particularly where sulfur loading fluctuates. However, automated injection is only as effective as the measurement point, control logic, calibration practices, and mechanical reliability behind it. Operators should validate that a control system is responding to the condition that matters, rather than merely maintaining a preset chemical rate.
Build a Response Plan That Holds Up in the Field
A written odor complaint procedure should be usable by the operator receiving a call at 2 a.m. Keep the workflow practical: capture the complaint details, assess immediate safety conditions, dispatch qualified personnel if needed, verify operating status, collect targeted measurements, and document corrective actions.
For recurring or high-consequence sites, include these four elements:
- A current source map identifying vents, tanks, process basins, loading points, and neighboring sensitive receptors.
- Defined escalation criteria for safety, environmental, maintenance, operations, and management teams.
- Minimum on-site inventory levels for critical treatment chemicals, pumps, instrumentation, and containment supplies.
- A post-event review process that identifies the cause, confirms corrective action, and updates operating procedures when needed.
Communication should be direct and proportionate. Do not speculate about causes before the investigation is complete. Share what is known, explain the steps being taken, and maintain records of timing, measurements, and corrective actions. This discipline supports regulatory discussions and helps demonstrate that odor concerns are being managed as an operational issue, not dismissed as a public-relations inconvenience.
Optimize Cost Without Creating a Repeat Complaint Cycle
The lowest unit-cost chemistry is not always the lowest-cost odor-control program. Chemical consumption, labor, equipment reliability, hauling, waste handling, downtime, corrosion exposure, and complaint management all affect the total cost of treatment.
Optimization often comes from improving the basics: placing injection where mixing is effective, maintaining pumps, preventing stockouts, matching dosage to loading, and separating true sulfur breakthrough from unrelated odor sources. In complex applications, field support can help convert variable process data into a treatment program that is both more dependable and more efficient.
Q2 Technologies approaches sulfur treatment as an operating system that combines application-specific chemistry, monitoring, injection optimization, and dependable field logistics. That approach is particularly valuable when odor performance depends on more than a drum of chemical.
Odor complaints are best handled before they become a pattern. A measured response, verified source data, and treatment adjusted to actual field conditions give operators a practical path to protect people, assets, and nearby communities while keeping the process under control.